Explore our elite spectrum of custom-manufactured athletic, functional, and retail-ready socks engineered for maximum durability and comfort.


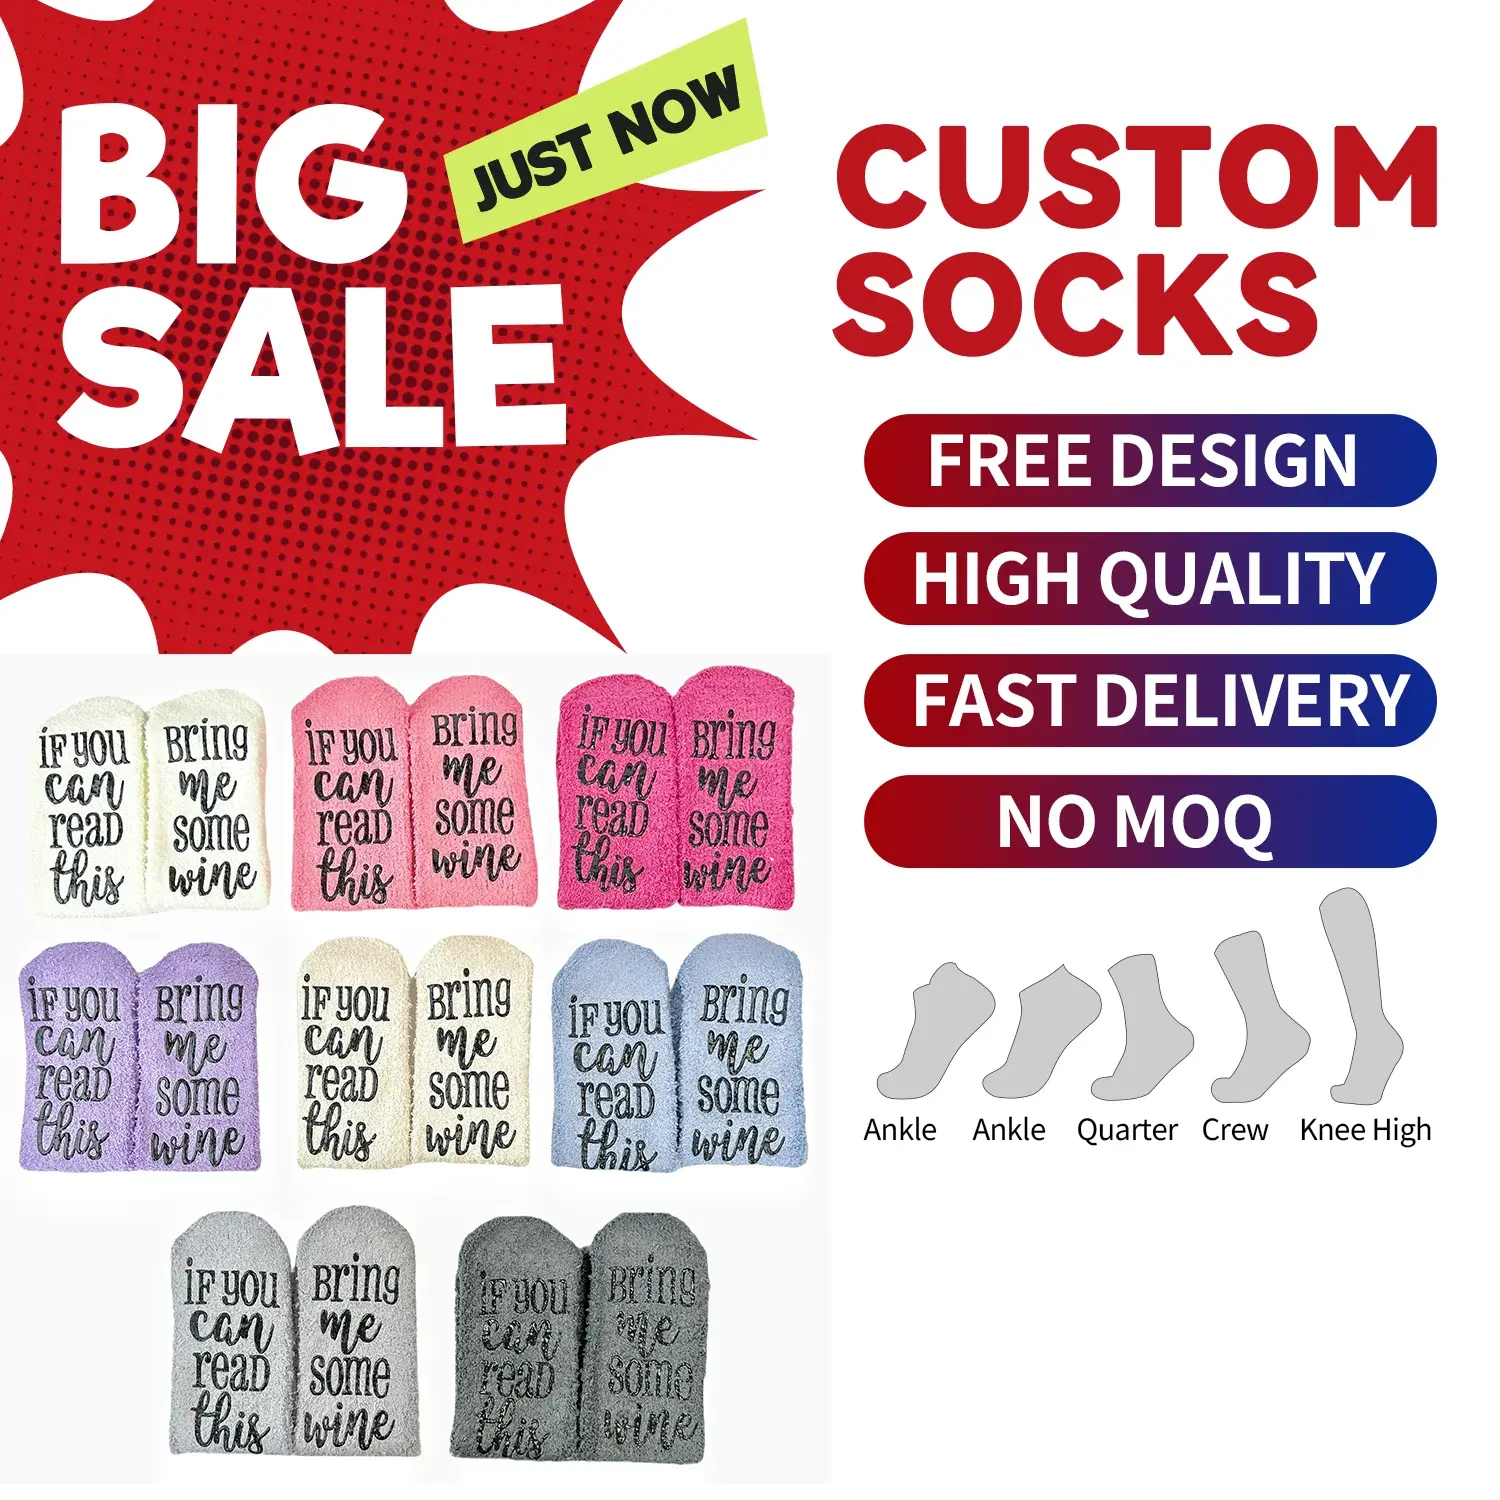
In the rapidly evolving global hosiery sector, wholesale red ankle socks have transitioned from traditional seasonal items into high-velocity year-round essential commodities across athletic, retail, corporate, and medical markets. Driven by shift in consumer intent toward vibrant color accents, ergonomic low-cut silhouettes, and moisture-regulating fiber blends, global demand for premium red ankle socks has achieved unprecedented momentum. Sourcing directors, brand owners, and wholesale distributors increasingly require manufacturing partners capable of balancing high-chroma dye fastness, structural yarn integrity, and rapid delivery schedules.
As a leading wholesale red ankle socks supplier and factory, Ningbo Cmax-Textile Co., Ltd has spearheaded innovation in high-density cylinder knitting, eco-friendly dye chemistry, and specialized functional weaves. Modern search intent mining reveals that commercial procurement teams do not merely seek low unit pricing; they demand deep technological capabilities, verifiable environmental compliance, and elastic supply chains resilient to macroeconomic fluctuations.
The global sports and lifestyle hosiery market is projected to reach $54.3 Billion by 2030. Red ankle socks represent a high-margin micro-segment growing at a CAGR of 6.8%, propelled by activewear styling, athleisure trends, and localized cultural celebrations.
Modern consumers demand "Invisible Utility"—socks that stay securely below the ankle collar without slipping, featuring targeted arch compression, mesh thermal regulation, and dynamic friction reduction to eliminate blisters during intense activity.
B2B purchasers require flexible OEM/ODM capabilities, ranging from exact Pantone color matching (such as Pantone 18-1664 TCX Scarlet Red) to specialized anti-slip silicone grip application and custom novelty packaging concepts.
Achieving a brilliant, saturated red hue on ankle socks without compromising tensile strength, breathability, or colorfastness requires rigorous chemical and mechanical control. Red dyestuffs historically present higher rates of bleeding and crocking if not processed with advanced reactive dye fixatives. At CMAX Textile, our laboratory engineering team implements a strict protocol ensuring Grade 4.5 colorfastness under ISO 105-C06 wash standards.
| Performance Parameter | Technical Specification | Engineering Benefit to B2B Buyers |
|---|---|---|
| Needle Count Range | 52N Heavy Duty Gauge to 320N Ultra-Fine Gauge | Versatility to manufacture thick winter slipper socks down to microscopic dress/sports ankle socks. |
| Yarn Matrix Blends | 32s/2 & 40s/2 Long-Staple Combed Cotton + Coolmax / Spandex | Optimal tactile softness paired with rapid moisture dispersion and high-elasticity shape memory. |
| Dye Chemistry | Azo-Free Reactive Red Dyestuffs (Oeko-Tex Standard 100 certified) | Zero skin irritation hazard, zero toxic runoff, compliant with European REACH regulations. |
| Toe Closure Tech | Automated Seamless Rosso Linking / Hand-Linked Toe | Eliminates toe ridge friction, preventing blisters and enhancing tactile comfort in athletic footwear. |
| Elastane Banding | Double-Covered Lycra Arch Support (15-20 mmHg zonal compression) | Prevents sock slippage into the shoe, decreases midfoot fatigue, and maintains elastic memory through 100+ wash cycles. |
Our red ankle sports socks utilize zoned micro-mesh knitting structures along the instep. This 3D breathable network creates a micro-climate chimney effect, transferring heat and perspiration vapor away from the foot surface 40% faster than standard carded cotton socks. Integrated Coolmax® and bamboo viscose fibers further accelerate capillary evaporation, keeping athletes dry and comfortable.
Driven by automated tech, decades of mastery, and uncompromising global quality standards.
Tailoring technical characteristics, fiber compositions, and visual branding to match diverse commercial eco-systems.
Designed for marathons, cross-training, and gym workouts. These red low-cut socks incorporate dynamic heel tabs (achilles protection pads), targeted terry cushioning under the heel and forefoot, and high-tenacity red polyamide yarns that withstand extreme abrasion friction tests (>50,000 Martindale rubs).
Red ankle socks serve as an iconic pop-color contrast accent in streetwear culture when paired with sneakers. We offer custom jacquard logo insertion, localized embroidery, rib-knit cuffs with micro-elastane retainers, and retail-ready header card packaging engineered for visual merchandising appeal.
Red is globally recognized as a symbol of celebration, good fortune, and energy. Our facility produces mass-quantity promotional red socks for Lunar New Year campaigns, Christmas retail lines, corporate marathons, and awareness events, supporting rapid turnarounds and high-volume delivery.
Utilizing extra-wide non-binding cuffs knitted on special 200N loose-tension cylinders, our red diabetic ankle socks feature smooth toe seams and full-cushioned soles. High-friction silicone gripper patterns can be customized on the sole for hospital and senior care safety.
Leveraging our famous creative packaging division, red ankle socks are rolled and presented as sushi rolls, pizza slices, cupcakes, or donuts. This unique packaging format creates high impulse-buy retail engagement and viral social media appeal for global boutique gift retailers.
Custom red open-toe or full-coverage ankle yoga socks with eco-friendly PVC or transparent silicone bottom tread dots. Engineered to provide maximum floor traction, lateral foot stabilization, and moisture absorption during high-intensity studio fitness sessions.
Strategic geographic location and vertical industrial cluster consolidation are vital for mitigating global supply chain risks. Ningbo Cmax-Textile Co., Ltd operates at the heart of Ningbo, China—home to the world's premier deep-water container port (Ningbo-Zhoushan Port). This geographic dominance provides direct shipping routes to major ports across North America, Europe, Australia, and Latin America, slashing maritime transit times and lowering freight overheads.
We maintain direct partnerships with spinning mills in Zhejiang and Jiangsu, locking in bulk contracts for combed organic cotton, GRS-certified recycled polyester, bamboo pulp yarn, and genuine Coolmax® fibers. This ensures raw material price stability even during global commodity inflation.
Our digital CAD design studio generates full-color technical sock mockups within 24 hours. Physical counter-samples, including custom dyed red yarn matching and logo weaving, are produced and dispatched via express courier within 3 to 5 business days.
Whether you are an emerging indie brand requiring low minimum order quantities (MOQ) of 500 pairs per size/color, or a multinational supermarket chain demanding 1,000,000+ pairs monthly, our 500+ machinery fleet dynamically adapts to your scale.
Established in the year 2000, Ningbo Cmax-Textile Co., Ltd has grown into a premier specialized garment accessory and hosiery producer and exporter in China. Over 25 years of relentless pursuit of quality and textile innovation, our manufacturing footprint covers 20,000 square meters, equipped with more than 500 advanced computer-controlled knitting machines spanning 52N to 320N cylinder gauges. Operating with a dedicated workforce of over 100 skilled production staff and 10 executive management members, CMAX achieves an annual export output value exceeding US $15 Million.
Headquartered near Ningbo Port, we provide comprehensive OEM and ODM customization services for global clients across the USA, European Union, Australia, Russia, Germany, Panama, Canada, and South Africa. Beyond socks, our specialized product menu includes slippers, footlets, tights, and thermal leggings—supplying many of the largest supermarket chains across Germany and North America.
As AI-driven automated textile manufacturing and smart wearables re-shape the apparel ecosystem, Ningbo Cmax-Textile is committing substantial R&D investment toward sustainable fiber innovation, automated quality control, and zero-waste production methodologies.
Transitioning toward 100% circular textile options. We are expanding our stock of GOTS-certified organic cotton, OCS-certified sustainable blends, Tencel™ Modal, biodegradable elastane, and recycled post-consumer PET nylon (GRS certified).
Integrating machine-vision camera arrays directly onto our 320N knitting machines. Real-time optical scanning detects dropped stitches, yarn tension irregularities, or dye spot variances instantly, reducing scrap rates to under 0.2%.
Pioneering supercritical CO2 dry-dyeing techniques for synthetic red yarns, drastically reducing industrial water consumption, chemical discharge, and energy requirements compared to conventional bath dyeing.
Global brand buyers and enterprise retail chains demand transparent compliance, non-toxic chemical guarantees, and verified ethical labor standards. CMAX operates with full audit clearance from leading international certification bodies.
Guarantees all red yarns, dyes, and elastic bands are free from harmful heavy metals, formaldehyde, and toxic aromatic amines.
Business Social Compliance Initiative certification ensuring fair wages, workplace safety, and ethical labor standards.
Verified supply chain transparency, social accountability, environmental stewardship, and business ethics.
Global Organic Textile Standard certification verifying organic cotton chain of custody from farm to finished sock.
Additional Facility Approvals: WRAP Certification, Disney FAMA License Standard, ISO 9001 Quality Management.
Clear, technical answers to common queries regarding wholesale red ankle socks sourcing, custom engineering, pricing, and shipping logistics.
Our standard MOQ for custom OEM/ODM designs is 500 to 1,000 pairs per design/colorway depending on the yarn specification and needle gauge (52N to 320N). For stock yarn colors or standard red shades (such as Pantone 18-1664 TCX), flexible lower MOQs can be accommodated to support boutique brands and promotional trials.
We utilize high-grade Azo-free reactive dyes combined with high-temperature color-fixation baths. Every batch undergoes ISO 105-C06 color fastness testing (rubbing and washing) to achieve a Grade 4.5 rating, ensuring zero dye transfer or color degradation even after repeated home laundering at 40°C.
For high-intensity sports, we recommend an optimized blend of 78% Combed Cotton (or Coolmax® polyester), 19% High-Tenacity Polyamide (Nylon) for heel/toe anti-abrasion durability, and 3% Lycra Elastane for dynamic midfoot arch support and shape recovery.
Absolutely! We are pioneer innovators in novelty gift sock packaging. We can fold, roll, and package your custom red ankle socks into sushi rolls, pizza boxes, cake boxes, donut packs, or beer cans, complete with custom printed branded bands and barcodes.
Digital CAD artwork mockups are provided within 24 hours. Physical samples with custom woven logos take 3-5 business days. Once the sample is approved, bulk production requires 15 to 25 days, supported by Ningbo Port’s fast sea freight and express air logistics options.
Discover our extended line of specialized diabetic, thermal, sports, and casual socks manufactured with high-precision Chinese supply chain capability.



 Cmax Textile
