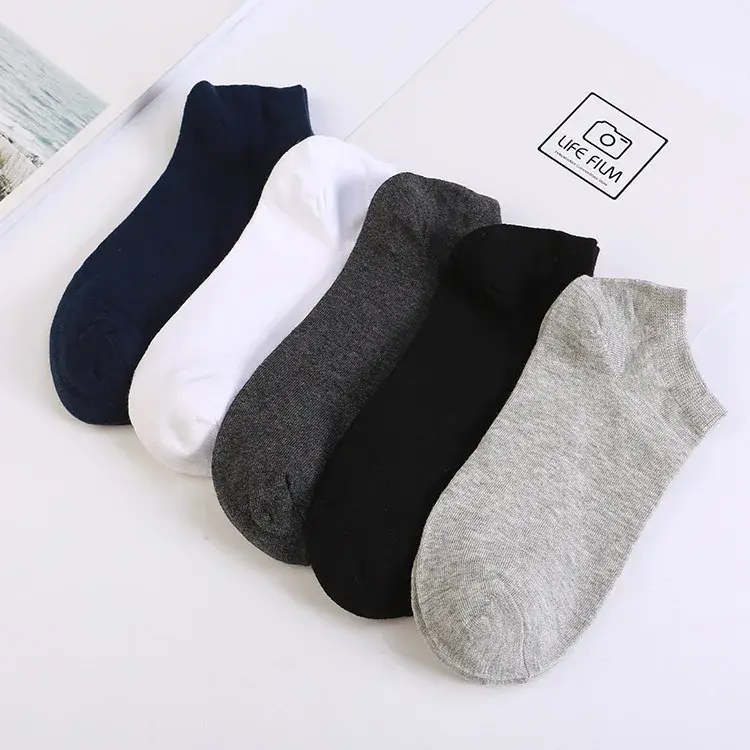
Explore our premium wholesale series engineered with advanced needle-gauge precision and ergonomic functionality.
An authoritative analysis of procurement shifts, technical yarn innovations, and supply chain agility in modern B2B textile trade.
The global hosiery and sock manufacturing sector is experiencing a monumental transformation. Commercial enterprise buyers, DTC apparel brands, and retail giants are moving beyond simple low-cost procurement toward multi-dimensional value metrics: high-density knitting capabilities, rapid custom sampling, eco-certified raw material tracing, and seamless OEM/ODM technical execution.
As international supply chains emphasize operational resilience, Ningbo, China has solidified its status as an indispensable global manufacturing nexus. Benefiting from state-of-the-art deep-water port infrastructure, mature raw material clusters, and advanced digitized production networks, Chinese manufacturers provide unprecedented scale and precision for bulk orders worldwide.
Modern consumers demand specialized features in everyday footwear accessories—ranging from moisture-wicking coolmax tech for marathon runners, to non-slip silicone traction for trampoline safety parks, and eco-friendly organic cotton for conscious daily wear. Furthermore, international regulatory frameworks (such as European ESG standards) require strict factory audits including OEKO-TEX®, BSCI, WRAP, SEDEX, and GOTS certifications.
Navigating these regulatory demands requires a manufacturing partner with proven technical expertise, robust quality management systems (AQL 1.5/2.5 inspection standards), and flexible production line configuration.
Engineered precision from 52N ultra-heavy thermal to 320N ultra-fine luxury dress hosiery.
Our expansive industrial plant houses over 500 state-of-the-art automated knitting machines spanning from 52-needle chunky thermal gauge up to 320-needle ultra-fine density. This enables total product coverage across compression wear, seamless tights, plush slippers, performance athletic socks, and high-detail jacquard fashion hosiery.
We translate raw client concepts into production-ready physical prototypes within 3 to 5 business days. With flexible low MOQ thresholds and streamlined manufacturing schedules, enterprise clients achieve accelerated time-to-market while maintaining strict brand consistency.
Headquartered in Ningbo—home to the world’s busiest port complex in cargo tonnage—CMAX delivers unmatched supply chain efficiency. Our strategic location eliminates inland transit bottlenecks, guaranteeing prompt, reliable containerized shipping to North America, Europe, Australia, and worldwide destination ports.
| Needle Count (Gauge) | Primary Product Applications | Yarn Density & Structure Features | Target Vertical Market Segment |
|---|---|---|---|
| 52N – 84N | Heavy Thermal Socks, Cozy Plush Winter Wear, Indoor Slippers | Thick loop terry, high insulation thermal acrylic & wool blends | Extreme Cold Retail, Outdoor & Cabin Brands |
| 96N – 120N | Work Boot Socks, Heavy-Duty Tactical & Cushion Sport Socks | Coarse gauge durability, high impact heel/toe reinforcement | Workwear, Safety Equipment & Tactical Supply |
| 144N – 168N | Standard Athletic Crew, Football/Soccer Grip Socks, Casual Cotton | Optimal balance between breathability, elasticity & pattern resolution | Sporting Goods Chains, Corporate Promotional Merch |
| 200N – 320N | Ultra-Fine Dress Socks, Seamless Mesh Couple Socks, Fine Tights & Leggings | High needle density, complex jacquard detail, soft hand-feel silk/modal | Luxury Fashion Brands, Premium Boutique Department Stores |
Established in 2000, Ningbo Cmax-Textile Co., Ltd has grown from a specialized workshop into a global powerhouse in custom sock manufacturing, thermal leggings, seamless tights, and indoor slippers. Spanning a modern manufacturing footprint of over 20,000 square meters with more than 100 skilled staff members and 10 executive management leaders, our continuous innovation has propelled our annual output value past US $15 million.
For over two decades, our team has combined an intense passion for colorful hosiery with groundbreaking design creativity. Beyond traditional apparel knitting, CMAX pioneered revolutionary packaged sock concepts—transforming everyday socks into visually striking food items such as sushi rolls, pizza slices, burgers, french fries, donuts, and beer cans. This creative packaging mastery allows global brands to create viral retail merchandise and high-margin gift offerings.
Full compliance with European and North American retail audits and yarn traceability standards.
We source specialized raw materials tailored to distinct client technical packs:
Our facility passes stringent social, environmental, and quality audits from world-renowned brands and supermarkets (e.g., major German chains):
These credentials ensure smooth customs clearance and zero-friction compliance for top-tier retail distribution.
For organic and recycled textile inquiries, we supply authentic transaction certificates to verify chain-of-custody:
Customized OEM solutions engineered for diverse commercial operations and consumer markets.
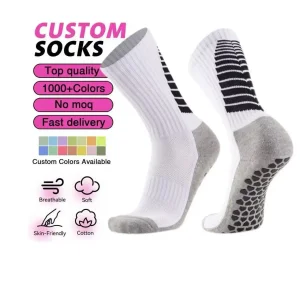
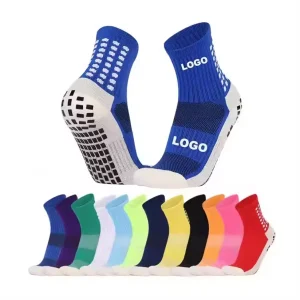
High-density cushioned bottoms, arc support bands, anti-slip silicone grip dots, and zonal mesh breathability designed for soccer, basketball, running, and cross-training athletes.
Specially formulated PVC/Silicone anti-slip grippers on child and adult sock soles to ensure maximum traction, safety compliance, and wash durability for commercial amusement parks.
Seamless high-waisted yoga pants, quick-drying compression leggings, and invisible no-show socks engineered for modern studio fitness and daily lifestyle wear.
Custom Jacquard logos paired with creative thematic packaging (Sushi boxes, Pizza slice triangles, Donut boxes) engineered to capture social media attention and boost impulse sales.
Discover more of our high-volume wholesale catalog manufactured to international standards.
Essential insights for procurement managers, brand owners, and global textile importers.
We pride ourselves on offer flexible MOQ thresholds to support growing brands as well as enterprise orders. Standard custom knit sock orders typically start at 500 to 1,000 pairs per design/colorway depending on yarn availability. For specialized custom-dyed Pantone yarns or complex technical builds, our team works closely with clients to accommodate optimal production batch sizes.
Physical sampling typically requires 3 to 7 working days upon receipt of tech pack or vector art. Once samples are approved, standard mass production turnarounds range from 15 to 25 days, facilitated by our fleet of 500+ high-speed automated knitting machines and direct access to Ningbo Port shipping channels.
Our manufacturing capabilities cover 52N, 84N, 96N, 108N, 120N, 144N, 156N, 168N, 200N, and up to 320N. Lower needle counts (52N-96N) create heavy, plush thermal or boot socks. Mid counts (144N-168N) are ideal for athletic crew and casual cotton wear. High needle counts (200N-320N) provide maximum pattern resolution and ultra-smooth hand feel for luxury dress hosiery and fine tights.
Yes. We possess verified GOTS (Global Organic Textile Standard) and OCS (Organic Content Standard) certifications. We can issue full transaction certificates (TCs) for organic cotton, recycled nylon, and recycled polyester lines to satisfy international import and retail verification compliance.
CMAX is world-famous for pioneered packaging designs including sushi rolls, pizza slice boxes, donut packs, burger boxes, and beverage cans. We also provide custom headcards, belly bands, eco-conscious recycled paper gift boxes, and display-ready retail cartons.
Our plant operates under strict AQL 1.5/2.5 quality control protocols. Every manufacturing batch undergoes 5 distinct inspection checkpoints: Raw Yarn Tensile Check, Knitting Loop Inspection, Hand-Linking/Toe-Seam Quality, Boarding/Heat Setting Symmetry, and Final Packaging Weight/Metal Detection Inspection.
 Cmax Textile